What Are Undercuts in Injection Molding? Types, Costs, and How to Design Around Them
Justin Brown
October 29th, 2026
Your mold quote comes back higher than you planned. One line item says “2 side actions.” You never asked for those, so where did they come from?
The reason is undercuts in injection molding. An undercut is a part feature that gets caught when the mold halves pull apart. To release it, the molder adds moving parts to the mold. Those parts add cost, and that’s likely why your quote went up.
Some undercuts are worth the cost. Others go away with a small design change. This guide explains what undercuts are and why they raise mold cost. It also shows how to keep the feature or design it out.
First, we’ll show you common undercut features and what they cost you. Next, we’ll explain the mold parts that form them, like side actions and lifters. Then we’ll cover design fixes for holes, windows, and clips. We’ll finish with the rare undercuts that are hard or impossible to mold.
What Are Undercuts in Injection Molding?
An undercut in injection molding is a feature that keeps a part from pulling straight out of a mold. Common examples are side holes, snap-fit hooks, threads, barbs, and windows in a side wall. External undercuts sit on the outside of the part. Internal undercuts sit inside it.
Undercuts can still be molded, but the mold needs extra moving parts to release them:
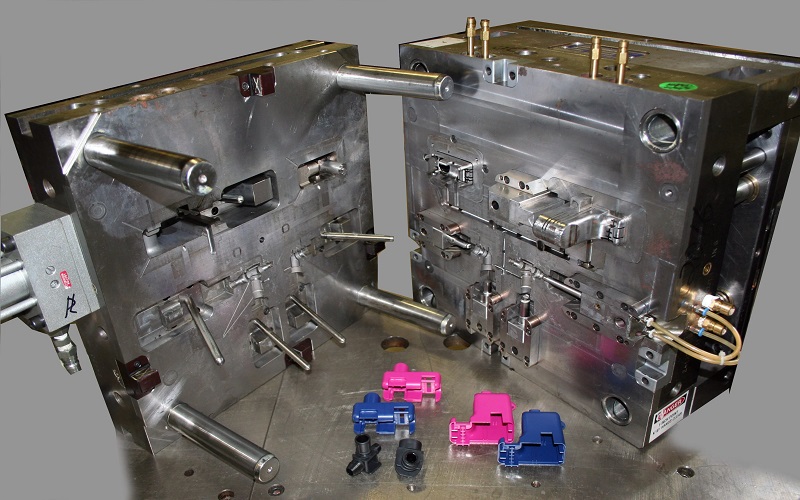
Side actions (slides) form features on the outside.
Lifters form features on the inside.
Hand-loaded inserts can work for short runs.
Each one adds cost and complexity to your tool. Many undercuts can be designed out instead. You can line the feature up with the mold pull, add a pass-through shutoff, or drill after molding.
What Counts as an Undercut? Common Undercut Features
You can spot most undercuts with one simple test. Imagine the two halves of the mold pulling straight apart. Does any feature on your part get caught on the steel? If so, that feature is an undercut.
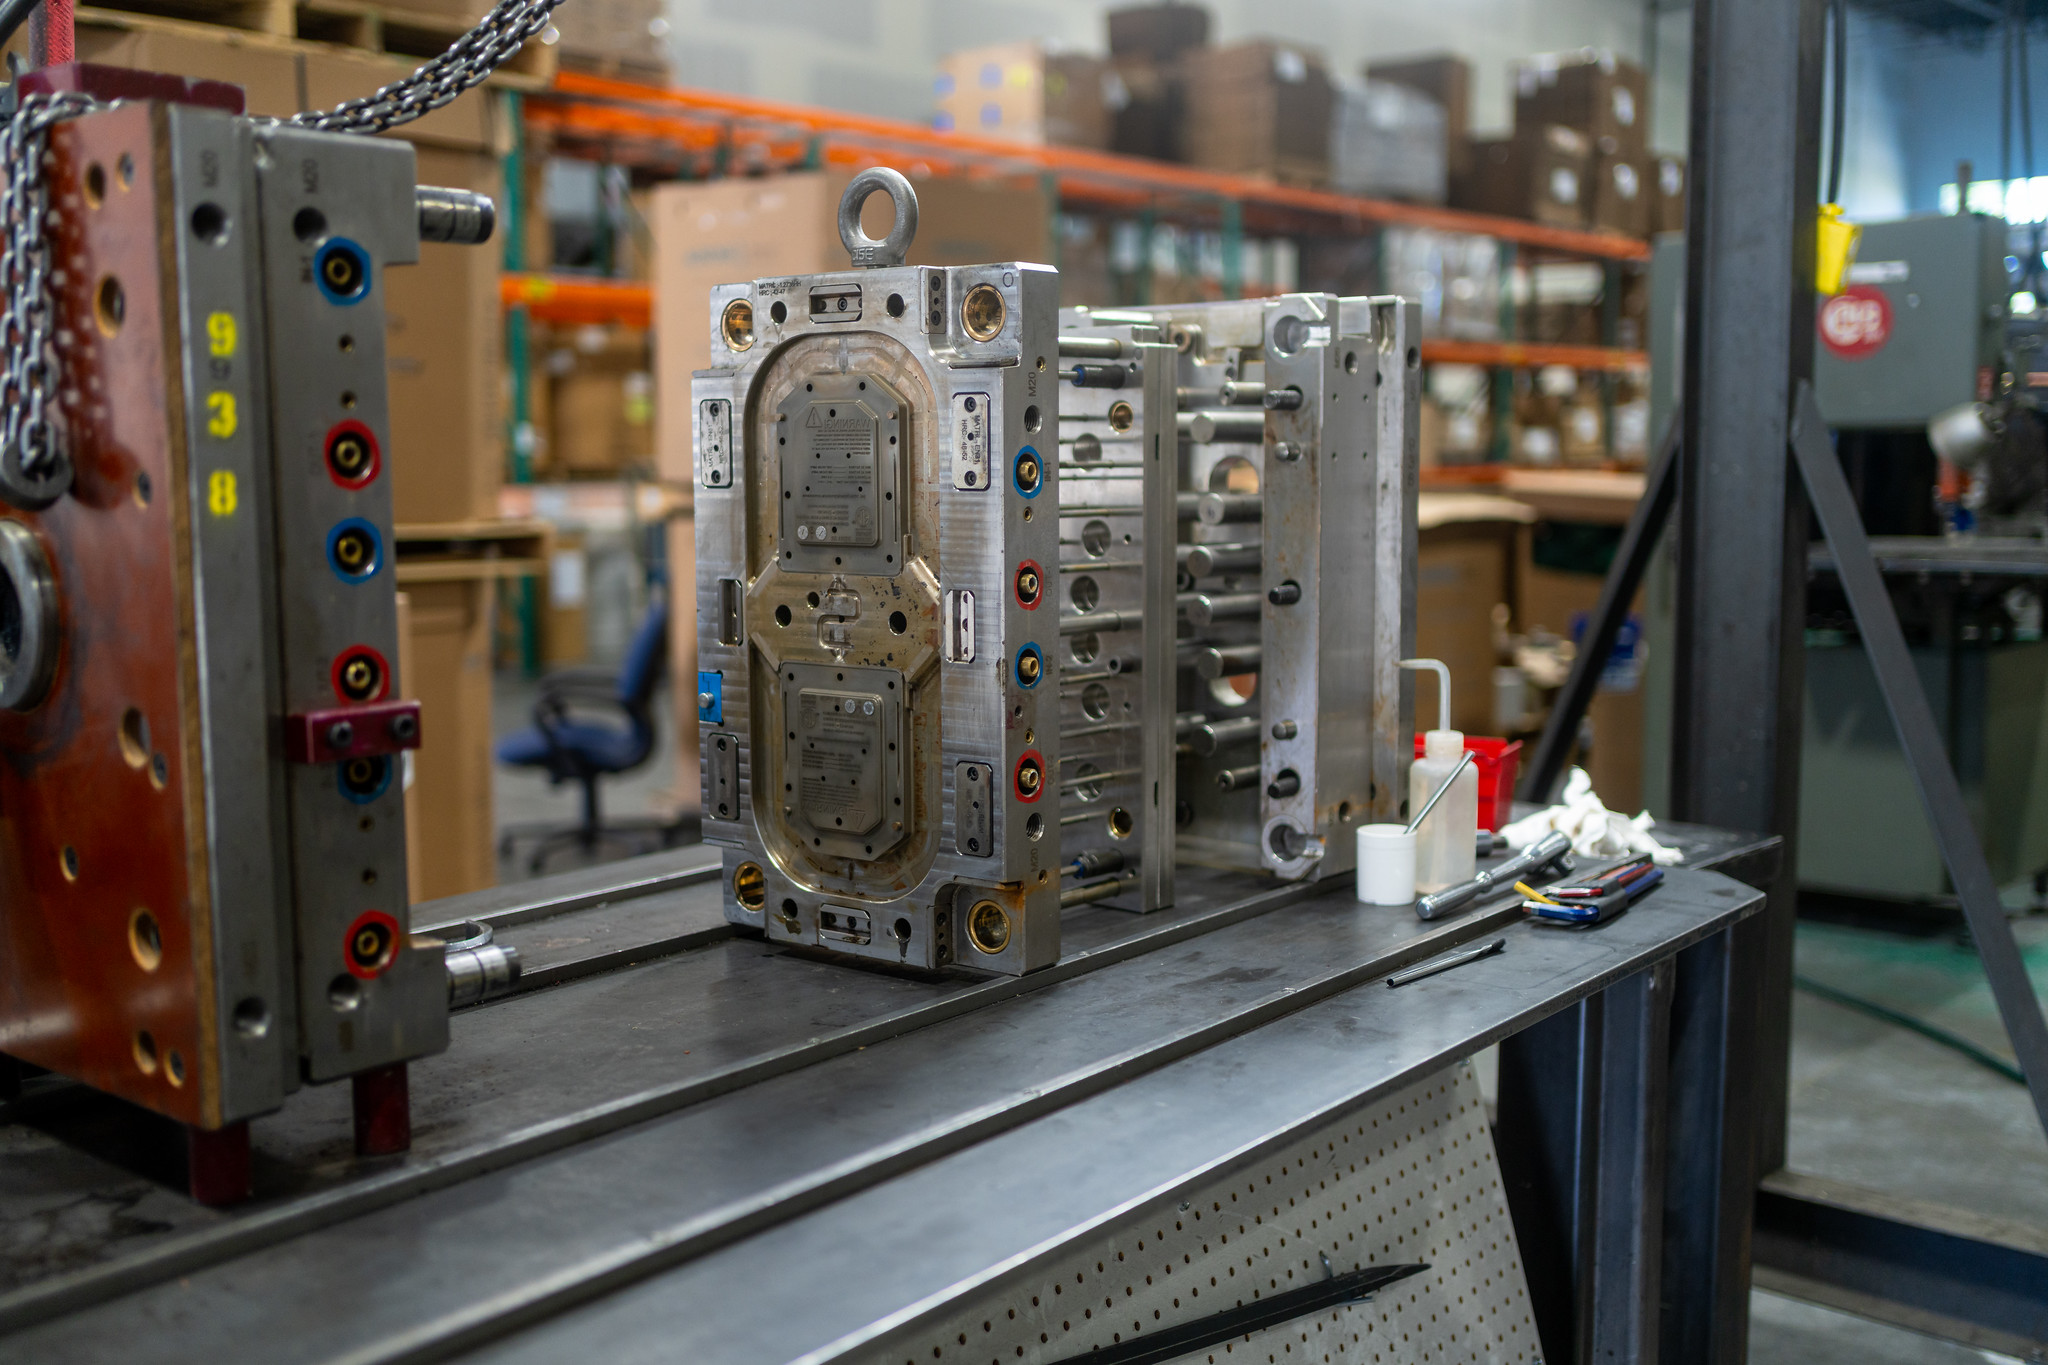
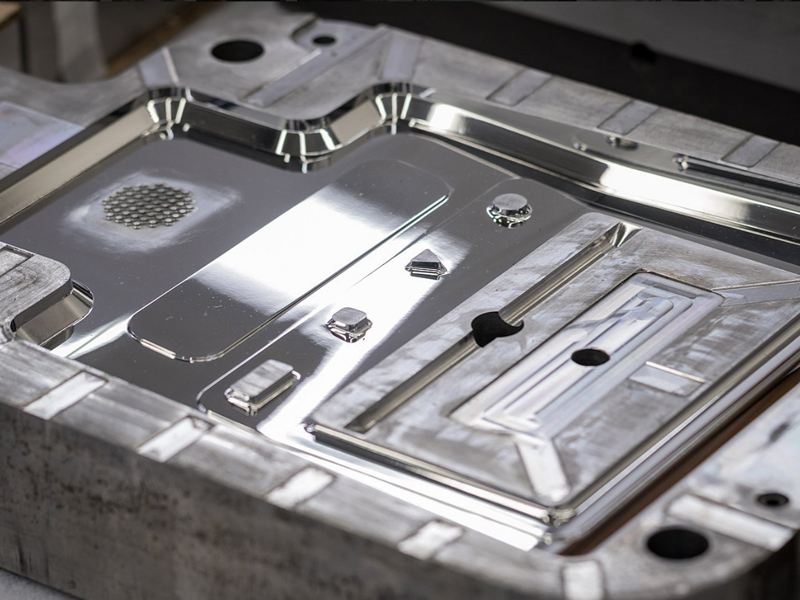
Most molds have two halves. The cavity forms the outside of the part, and the core forms the inside. Undercuts can show up on either side.
An external undercut sits on the outside of the part. A hole through the side wall of a box is a good example. An internal undercut sits on the inside. Threads inside a bottle cap are a common one.
Every undercut needs a part of the mold that moves on its own. That moving part has to be designed, cut from steel, and fitted into the mold. All of that shows up on your quote.
The main cost drivers are:
More steel for the slides, lifters, or inserts
More machining time to build and fit them
A longer build before your first parts ship
How much more? That depends on the part, the number of actions, and the size of the tool. Each action you add raises the price again. To see what else shapes your price, read our guide on what drives mold cost.
Moving parts also wear over time. Worn slides and lifters need repair or replacement over the course of a mold’s life.
Slide shutoff areas are a common spot for flash. Flash is a thin fin of extra plastic that leaks out between steel faces. As slides and lifters wear, small gaps can grow and make flash more likely.
That doesn’t mean you should avoid every undercut. It means you should decide on purpose. If the feature stays, here are the mold parts that make it possible.
How Molders Form Undercuts: Side Actions, Lifters, and More
If your quote lists side actions or lifters, these are the mold parts it means. Each one solves the same problem in a different way. The right choice depends on where the undercut sits and how many parts you need.
Side actions (slides) handle features on the outside of the part. They move in from the side, at a right angle to the way the mold opens. Angled pins guide them in as the mold closes and pull them back as it opens.
Lifters handle features on the inside of the part. As the part is pushed out, the lifter moves forward and sideways at the same time. That sideways motion pulls it free of the inner feature.
Hand-loaded inserts are loose metal pieces. An operator places one in the mold before each shot. It comes out with the part and is then removed. Inserts cost less to build but add time to each cycle, so they fit short runs.
Collapsible and unscrewing cores form threads on the inside of a part. A collapsible core shrinks inward to release the threads. An unscrewing core turns to back out of them.
Bump-offs work for small undercuts in flexible plastics like TPE, polyethylene, and polypropylene. The part flexes just enough to pop off the steel as it ejects. The undercut needs a rounded or ramped edge, not a sharp hook. No side action is needed.
Method
Best for
Cost impact
Run size fit
Side actions (slides)
Outside features like side holes and windows
Moderate to high
Low to high volume
Lifters
Inside features like inner clips
Moderate to high
Low to high volume
Hand-loaded inserts
Simple features on test or early parts
Low tool cost, slower cycles
Short runs
Collapsible or unscrewing cores
Threads on the inside of a part
High
High volume
Bump-offs
Small, rounded undercuts in flexible plastics
Low
Low to high volume
How to Design Undercuts Out of Your Part
Before you pay for a side action, check whether a small design change can remove the undercut. These fixes are far easier to make in CAD than in steel. Here’s how they work for the three most common problem features.
For Side Holes
A hole through a side wall stops the mold from opening straight. You have two ways around it:
Turn the hole so it runs the same way the mold pulls. The steel can then form it without moving sideways.
Mold the wall solid and drill the hole afterward. We offer post-mold machining in-house, so you don’t need a second vendor.
Drilling adds a step to each part. It fits best when a side action would cost more than that extra step.
For Windows and Slots
A window in a side wall usually calls for a side action. A pass-through shutoff can replace it.
One mold half reaches through the other to form the opening.
No sideways movement is needed, so the mold stays simpler.
The shutoff faces need at least 3 degrees of draft. Draft is a slight taper that helps the part slide off the steel.
For Snap-Fit Clips
The hook on a snap-fit clip catches on the steel when the mold opens. Two fixes can help:
Add an opening in the wall under the hook. A pass-through core can then reach through and form the hook straight up and down.
If the catch is small with a rounded or ramped edge, a bump-off may work in flexible plastics. Sharp hooks tend to stick in the mold or tear.
When an Undercut Can’t Be Molded
Most undercuts can be molded with the right mold parts. A few can’t, or cost too much to be worth it. These cases come down to space, because the steel needs room to move.
Undercuts that are hard or impossible to mold include:
Deep features inside a part, where a slide or lifter can’t travel far enough to clear them
Fully enclosed hollow shapes, where solid steel can’t get in or back out
Crowded inner walls, where a lifter would run into other features as it moves
Mold the part without the feature and machine it in afterward.
Rethink the shape so the feature points the way the mold pulls.
The earlier you know which route fits, the less it costs to change course.
Get Your Undercuts Reviewed Before the Steel Is Cut
An undercut is cheap to fix in CAD. Once the steel is cut, the same fix can mean new mold parts, rework, and delays. The best time to ask about undercuts is before your mold is built.
At our Logan, UT, shop, we handle DFM review, mold design and build, and post-mold machining in-house. Our team can flag the undercuts in your CAD and help you decide which ones to keep. For the rest, we’ll suggest design changes that keep your tool simpler.
We’ve served businesses across Northern Utah and Southern Idaho since 2011. Our shop is ISO 9001:2015 certified, so your parts are made under a documented quality system.
Ready to have your part checked? Contact us to request a quote or call us at (435) 774-9090 to get started!
Your mold quote comes back higher than you planned. One line item says “2 side actions.” You never asked for those, so where did they come from? The reason is…
You need 400 parts for a product launch. The first quote comes back with a 10,000-part minimum. Now you face a hard choice. You can buy parts you don’t need,…
Your circuit boards are finished. Your enclosure is molded. Screws, cables, and labels are coming from four different suppliers. Someone still has to turn that pile of parts into one…
You asked for a smooth, nice-looking part. Then the samples came back shiny, and every fingerprint and tiny dent showed. The mold did exactly what it was told. It just…
Your first sample parts look great until you flip one over. There’s a rough nub right on the face your customer sees first. That nub is where the plastic came…
Your first sample parts just came back. They look right until you tilt one toward the light. Then you see it: a shallow dent sitting right over a rib. Nothing…