What Is the Typical Tolerance for Injection Molding?
Your CAD model says 25.00 mm. Your first molded parts come back at 24.93 mm. Is that a problem, or is it normal? The answer depends on the tolerance you…
Your CAD model says 25.00 mm. Your first molded parts come back at 24.93 mm. Is that a problem, or is it normal?
The answer depends on the tolerance you called out on your drawing. It also depends on whether that number was realistic for plastic.
Cost plays a part too. The tightest numbers on your drawing can raise your mold price. Tightening a callout past what your part needs adds tooling cost with no benefit to the end user.
So, what is the typical tolerance for injection molding? Below, we give you the numbers and the factors that change them. Then we show you how to spec your drawing so parts fit without overpaying.
We start with the three tolerance classes: commercial, standard, and fine. Next, we cover how material, part design, and tooling and process control move those numbers. Last, we walk you through how to write tolerance callouts on your drawing.
The typical tolerance for injection molding is about ±0.005 inch (±0.127 mm) on small, well-controlled features. Molded tolerances are often grouped into three levels:
Some precision molds can hold ±0.001 inch on a few select features. That number does not apply across a whole part. Tolerances also loosen as parts get larger. Material shrink, wall thickness, and mold quality all change what is possible for your part.
A tolerance is the allowed range around a dimension on your drawing. Say your print calls for 25.00 mm ±0.13 mm. Any part that measures between 24.87 mm and 25.13 mm passes. The 24.93 mm part from earlier would be in spec.
Plastic shrinks as it cools in the mold. That means a molded part never matches your CAD model exactly. A tolerance tells your molder how much difference the part can handle and still work.
There are two main kinds of tolerance:
Tolerances are set per feature, not per part. A snap-fit tab may need a tight callout. The outside edge of a cover may not. You decide where precision matters, and the mold is built around those choices.
Molded tolerances are often grouped into three classes. Each class fits a different kind of feature on your part.
| Class | Inch | mm | Typical Use |
| Commercial | ±0.010 | ±0.25 | Non-critical features, such as outside edges and cosmetic surfaces |
| Standard | ±0.005 | ±0.127 | Most functional features on most parts |
| Fine | ±0.002–0.003 | ±0.05–0.08 | Critical fits, with tighter tooling and process control |
You may see ±0.001 inch quoted as possible. That number is real, but only on a few select features. It takes precision tooling and close process control. It is not something you should expect across a whole part.
Size matters too. A ±0.005 inch callout is realistic on a small feature. On a long dimension, the same number gets much harder to hold. Tolerances widen as dimensions grow because larger features shrink more in total.
Industry standards give you a shared language for these numbers. ISO 20457 covers tolerances for molded plastic parts. It replaced older German standards for molded parts, including DIN 16901.
Some features need more than molding can give. Tolerances tighter than about ±0.025 mm (±0.001 inch) usually call for precision machining after molding. For those features, the part is molded close to size and then machined to final spec.
Those numbers are starting points. The first thing that moves them is the plastic itself.
Every resin shrinks at its own rate as it cools. Semi-crystalline resins, such as polypropylene and nylon, tend to shrink more than amorphous resins, such as ABS and polycarbonate. Low-shrink resins are easier to hold to tight numbers. High-shrink resins give you a wider range to plan around.
Nylon has one more quirk. It absorbs moisture, so parts can swell after molding. A nylon part that measures right on day one may change size later. If your fit is tight, plan for that before you pick the material.
| Resin | Typical Tolerance (inch) | Typical Shrink Range |
| ABS | ±0.005–0.010 | 0.4–0.8% |
| Polycarbonate (PC) | ±0.005–0.010 | 0.5–0.7% |
| Polypropylene (PP) | ±0.005–0.015 | 1.0–2.5% |
| Nylon (PA) | ±0.005–0.015 | 0.5–2.0% |
*These are general reference ranges. Grade, fillers, and processing change the real values. Always check the resin maker’s data sheet for your exact grade.
Material sets the range. Your part design decides where in that range you land.
A few design choices make the biggest difference:
If a tight feature sits in one of these tricky spots, a small design change can often help. It is easier to adjust the part now than to fight it in the mold later.
The same part design can hit or miss its tolerances depending on the mold and the process behind it. That is why your choice of molder matters.
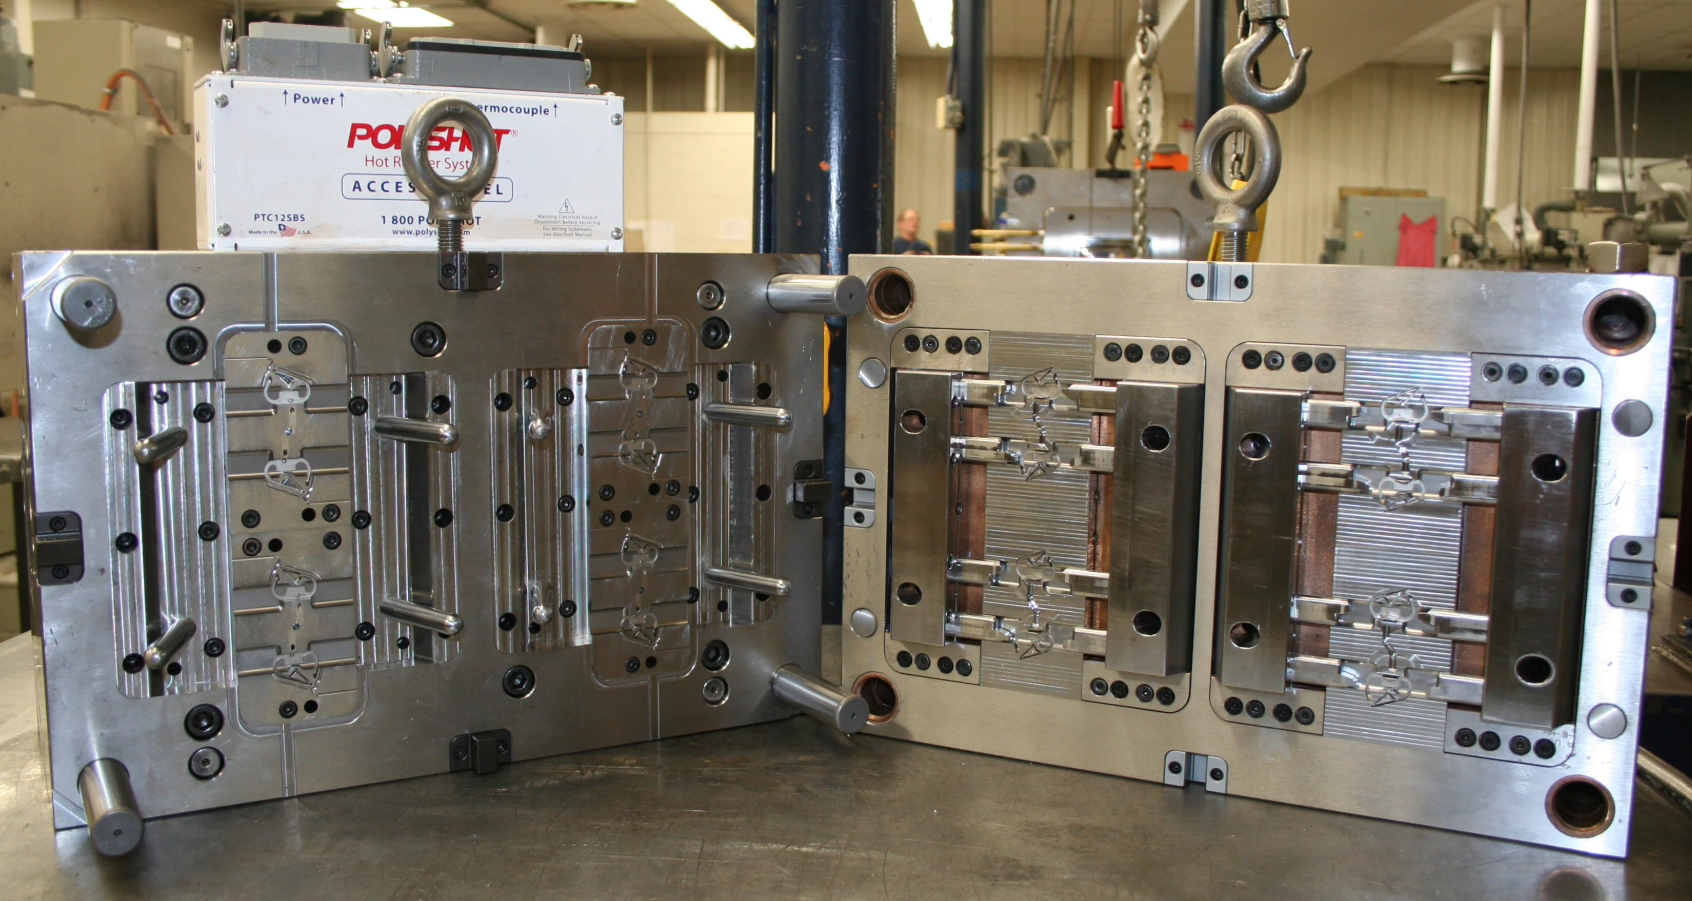
Steel vs. aluminum molds: Hardened steel molds resist wear better than aluminum molds, so they hold their size over more cycles. Aluminum works well for prototypes and short runs. For long runs with tight callouts, steel keeps your parts in spec longer.
Mold layout also plays a part. A multi-cavity mold makes several parts per shot, but parts from each cavity can differ slightly. That adds cavity-to-cavity variation you have to plan for.
Repeatable parts come from steady cooling and stable process settings. A well-placed cooling layout helps each part shrink the same way. Locked-in settings keep shot 10,000 close to shot 10.
Before production starts, we run molds through staged trials known as T0, T1, and T2. The first trial checks how the mold moves and functions, and the next ones check real parts. Every trial is documented, and every change to the tool or process is tracked. We sign off a mold only after it meets the criteria set at the start of your project.
Our ISO 9001:2015 certified quality system keeps that same discipline from one run to the next. Your tenth order should measure like your first.
Knowing what’s possible is half the job. The other half is writing it on your drawing the right way.
Use this checklist before you send your print out for quotes:
A careful drawing gets you accurate quotes and parts that fit the first time.
When your part has tight callouts, it helps to have every step under one roof. At our shop in Logan, we handle design review, mold making, molding, and machining in-house. Your drawing, your mold, and your parts stay with one team from start to finish.
Here is what that means for your tolerances:
Our ISO 9001:2015 certified quality system backs every run. We work with companies across Utah and even beyond that need local, reliable parts.
Ready to see what your part can hold? Learn more about our custom plastic injection molding or call us at (435) 774-9090 to get started!